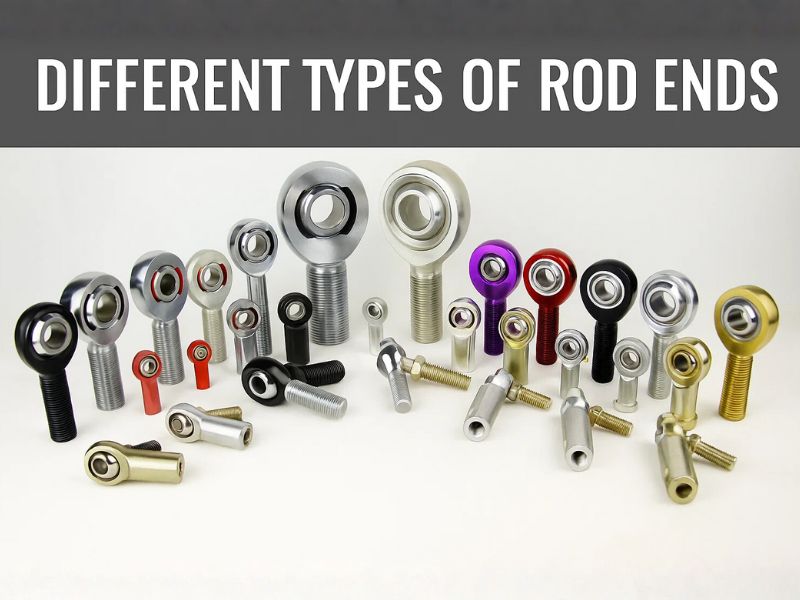
A rod end that looks right on the spec sheet can still fail early if its structure or lining doesn't match how the joint actually loads and moves. Most selection mistakes trace back to one of three decisions: two-piece versus three-piece construction, lined versus metal-to-metal contact, and a material chosen for cost instead of the operating environment. Get those three right and the rest of the spec sheet mostly takes care of itself.
How Rod End Type Affects Failure Mode
Rod ends rarely fail all at once. They loosen up first. Play develops at the ball-to-race interface, then noise, then the housing or thread starts taking loads it wasn't designed for. Which failure mode shows up first, and how fast, depends on the type you picked:
- Metal-to-metal designs wear gradually as the ball rides directly on the race. Without lubrication, that wear accelerates under vibration or dust ingress.
- PTFE-lined designs resist wear differently: the liner absorbs the sliding motion instead of the metal surfaces. They run maintenance-free until the liner degrades from heat or contamination, at which point wear resumes quickly.
- Greaseable designs depend on the maintenance schedule actually happening. Skipped relubrication is one of the most common causes of premature failure in agricultural and construction equipment.
Knowing which failure mode you're trying to avoid, gradual wear, liner degradation, or missed maintenance, is a faster way to pick a type than starting from a materials list.
Two-Piece, Three-Piece, or Injection-Molded: Which Handles Your Load
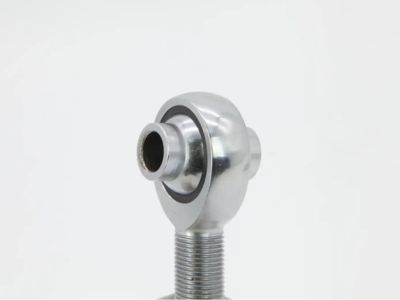
Two-piece rod ends are the simplest design: a ball riding directly in a formed housing, no separate race. They handle a wide misalignment range, commonly in the range of 15° to 25° depending on the specific design, and cost less. They're the right call for A-arms, trailing arms, and radius rods where the load is mostly static or slow-cycling and periodic inspection is realistic.

Three-piece rod ends add a separate race between the ball and housing. That extra part improves load distribution and gives the joint a longer fatigue life under repeated cyclic loading, which is why they show up in shifter linkages, sway bar assemblies, and other high-cycle racing applications. The tradeoff is more parts and a higher cost.

Injection-molded rod ends use a molded liner, commonly nylon, between the ball and housing instead of PTFE or bare metal. They're light and require no lubrication, but the liner absorbs moisture and can swell. Don't spec an injection-molded type for a wet or washdown application; a PTFE-lined or stainless metal-to-metal design holds up better there.
Matching Material to the Operating Environment
Material choice matters more than most spec sheets suggest, because the failure modes above compound with corrosion, temperature swings, or fatigue depending on what the rod end is made of.
- Carbon steel is the default for indoor machinery and standard automotive linkages. Zinc or chrome plating gives basic corrosion resistance, but that plating wears through, and salt spray or high-humidity service shortens service life fast once it does.
- Chromoly steel trades some corrosion resistance for higher fatigue strength and lower weight, which is why it's common in custom control arms and steering linkages built for repeated impact loads. It still needs a real surface treatment; chromoly on its own corrodes.
- Stainless steel skips the plating question entirely. It costs more up front but holds up in mud, salt spray, and humidity without a coating to maintain, which is why it's the standard choice for marine hardware and outdoor industrial equipment that can't be taken out of service for recoating.
- Aluminum cuts weight where the load is light and the priority is responsiveness, such as sway bar links on a race car. It has lower fatigue strength than steel, so it's the wrong choice for a high-load or high-cycle joint regardless of how much weight it would save.
- Titanium combines low weight with high fatigue resistance, which is why it shows up in aerospace and top-tier racing where both matter and cost is secondary.
- Plastic rod ends are self-lubricating and cheap but low-strength. They belong on light linkages, not load-bearing joints.
Heim Joint or OEM-Style Tie Rod End
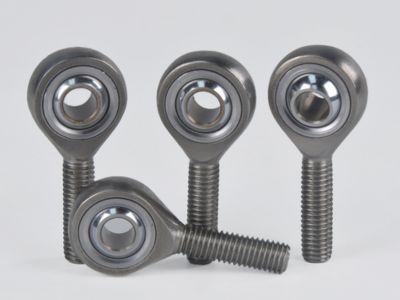
This is the question that actually decides most builds, and it gets less attention than the materials list. A heim joint (the two- or three-piece rod end styles above) gives you more articulation and is easy to inspect and replace. An OEM-style sealed tie rod end lasts longer in daily driving because the boot keeps contaminants out, but it's harder to source in custom sizes and doesn't articulate as far.
Exposed heim joints wear faster than sealed tie rod ends under the same mileage, because nothing is keeping dust and moisture off the joint. That's an acceptable tradeoff on a race car serviced between events. It's usually the wrong call on a daily driver, where a sealed tie rod end will outlast a heim joint by a wide margin and won't develop the clicking or play that shows up in exposed joints after a season of use.
Common Failure Causes, and Which Type Prevents Each
- Insufficient lubrication is the leading cause of failure in greaseable designs specifically; a PTFE-lined type removes this risk entirely by not needing a lubrication schedule.
- Contamination from dust or water accelerates wear in any exposed metal-to-metal joint; a sealed OEM-style tie rod end or a stainless PTFE-lined rod end resists this better than an open two-piece design.
- Overload happens when a joint rated for static load gets used in a high-cycle application; that's a three-piece-versus-two-piece decision, not a material decision.
- Assembly error, wrong torque or a misaligned installation, causes premature failure regardless of type and is worth checking first when a joint fails early.
Thread, Bore, and Temperature: The Dimensional Checks That Get Skipped
Getting the type and material right doesn't help if the part doesn't fit the joint. A few dimensional checks catch most of the ordering mistakes we see:
- Male vs. female thread. A male rod end has external threads and screws into a tapped bracket or clevis. A female rod end has an internal bore and takes a bolt or stud through it. Check which one the existing hardware expects before ordering a replacement.
- Right-hand vs. left-hand thread. An adjustable linkage, a tie rod or a turnbuckle-style link, needs one right-hand and one left-hand rod end on opposite ends so the assembly lengthens or shortens when you rotate the center tube. Ordering two of the same hand means the link can't be adjusted at all.
- Imperial vs. metric. UNF/UNC threads dominate North American aftermarket and off-road builds; metric M-series is standard on European OEM equipment. Mixing the two on the same joint strips threads on both parts, not just one.
- Bore diameter to pivot bolt. The bore needs to match the pivot bolt's actual diameter, not just its nominal size. An oversized bore introduces play immediately; an undersized one binds and pre-loads the joint before it ever sees an operating load.
Lining type also sets a real operating temperature ceiling, not just a maintenance schedule. A PTFE-lined rod end built to SAE AS81820 is rated for -65°F to 325°F (-54°C to 163°C), which covers most industrial and outdoor use, but it's still a ceiling. A greaseable metal-to-metal design tolerates less cold before the grease stiffens and more heat before it needs to be re-lubricated on a shorter cycle, and a dry metal-to-metal design (no grease, no liner) has the widest tolerance of the three but wears fastest without one.
Conclusion
Start with how the joint fails if you get it wrong, not with a materials list. Confirm two-piece, three-piece, or injection-molded based on load cycling and misalignment range. Confirm heim joint or sealed tie rod end based on how much articulation you actually need versus how long it has to last unattended. Then pick the material for the environment, not the catalog price.
Profab Machine manufactures stainless steel rod ends in two-piece, three-piece, and PTFE-lined configurations across 304, 316L, and 17-4PH, built for marine, food-processing, and industrial applications where a coated carbon steel rod end won't hold up.