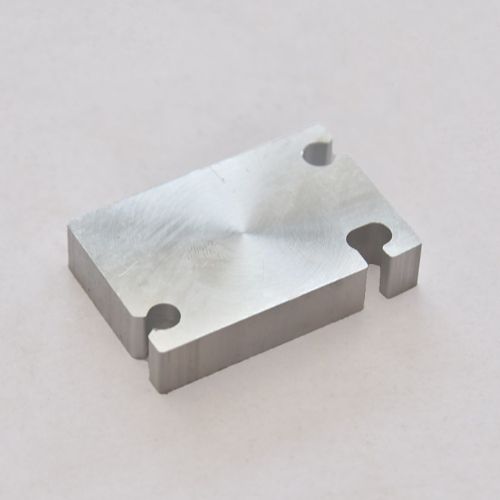
Flat and Pocketed Plates
Typical features
Faced surfaces, pockets, slots, and drilled hole patterns.
Drawing should show
Plate thickness, pocket depth, and hole positions from one datum.
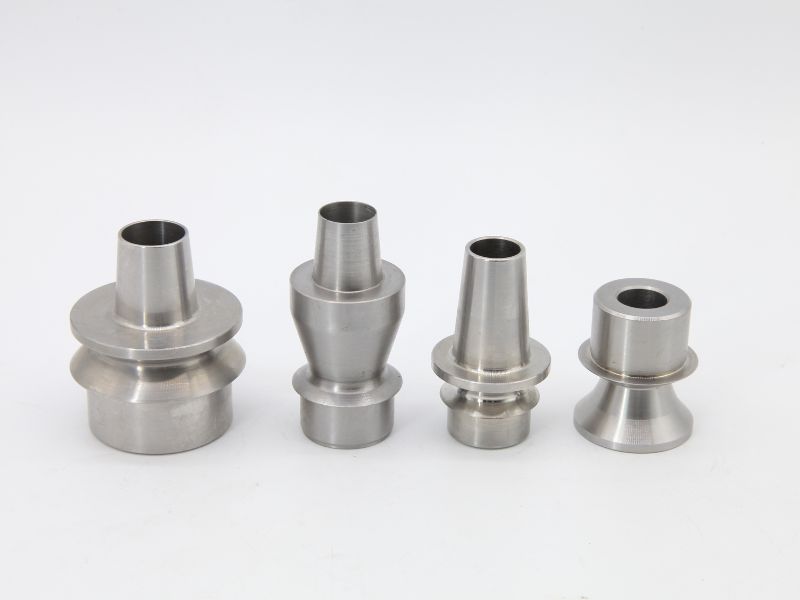
Profab machines stainless steel parts to your drawing at our CNC shop in Fenghua, Ningbo. They range from brackets, housings, and plates to round parts with milled features. A sample or a worn part also works as the starting point.
Send STEP, IGES, DXF, DWG, or PDF drawings, or a physical sample.
CNC machining cuts flats, pockets, slots, holes, and round profiles into bar or plate. Each card lists the usual features of a part type and what your drawing should show.
Faced surfaces, pockets, slots, and drilled hole patterns.
Plate thickness, pocket depth, and hole positions from one datum.
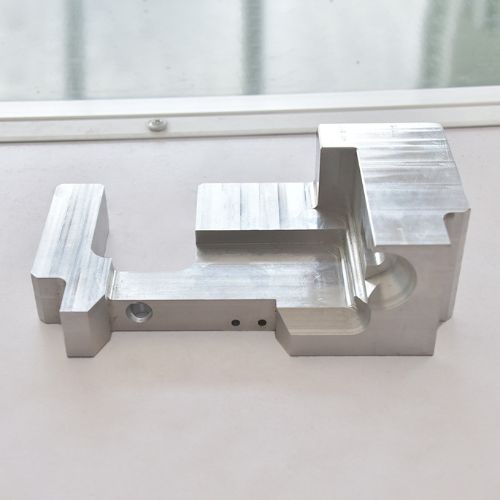
Steps, slots, and holes cut on several faces of one block.
A datum scheme and the angle between faces.
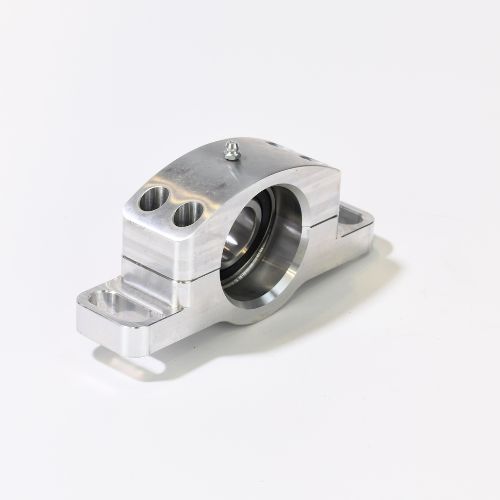
A bored seat, a split line, and a bolted mounting base.
Bore size and fit, bolt pattern, and the height to the bore center.
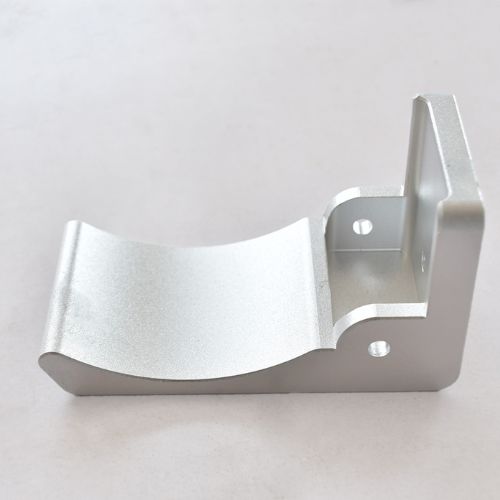
Upright legs and curved seats cut from solid, with mounting holes.
The seat radius, the angle between legs, and the hole positions.
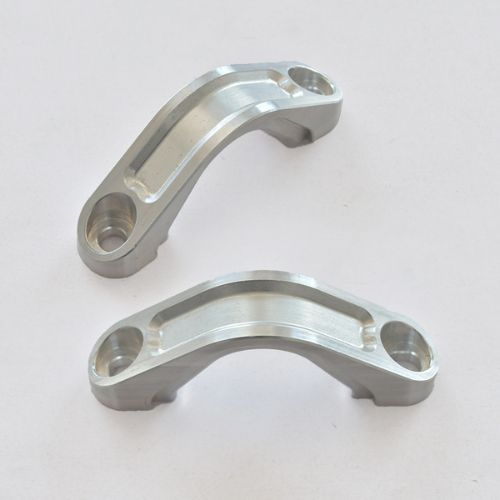
Curved outlines, slots, chamfers, and blended edges.
The contour as a STEP or DXF file, plus the edge break.
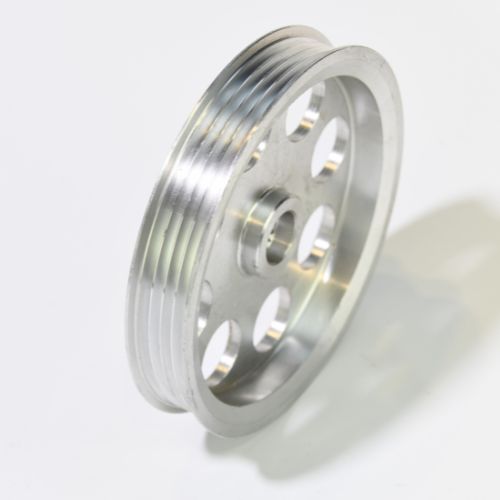
Turned bodies finished with face holes, flats, or slots.
Which features are milled after turning, and where they sit.
5-axis machining is available on request when angled features need it. Send a STEP file with the drawing for those parts.
Round parts such as pins and shafts are covered on our CNC turning parts page. Stamped and bent parts have their own sheet metal parts page.
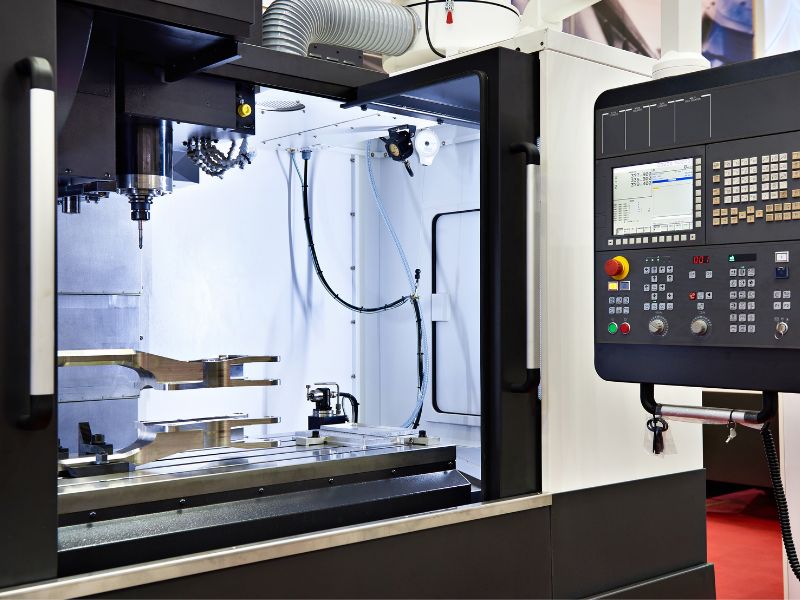
Mark the dimensions that matter. We plan the setups around them.
What a feature can hold depends on its size, its shape, and the grade.
Choose the grade by where the part works. The last column says how each one behaves under the cutter.
| Grade | Minimum yield strength | Pitting resistance (PREN, typical) | Machining note |
|---|---|---|---|
| 304 | 205 MPa | 18 to 20 | Cuts cleanly. The usual choice for dry and fresh-water parts. |
| 316L | 170 MPa | 24 to 26 | Gummier to cut than 304. Chosen for wet, washdown, and welded parts. |
| 17-4PH (H1025) | 1000 MPa | Lower than 316L | Strong and hard. Heat treatment is available on request. |
| 303, duplex 2205 and 2507 (on request) | Depends on grade | Depends on grade | 303 cuts freely for dry parts. Duplex suits chloride service under load. |
Swipe to see all columns
Values are typical minimums for annealed plate and for 17-4PH in the H1025 condition, given for comparison.
Other metals are available on request.
Each step carries a tag for where it happens. Steps marked on request or we offer are added only when your part needs them.
Bar or plate is sawn to a blank with machining allowance.
Round profiles are turned. Faces, pockets, slots, and contours are milled to your drawing.
Holes and threads go in next. A ground finish is used where a face needs a tighter size.
17-4PH and other hardenable grades can be heat treated after machining.
Passivation and electropolishing clean the surface. Other finishes, such as blackening, are available on request.
Four features raise most of the questions we ask during quoting. A note on the drawing settles them early.
A milled inside corner takes the radius of the cutter. Give each inside corner a radius, and make it larger where the part allows.
A thin wall can vibrate and move while it is cut. Deep pockets need long tools, which flex. Keep walls as thick as the function allows.
Stainless steel hardens at the surface when a dull tool rubs instead of cutting. For dry parts with heavy machining, the free-cutting grade 303 is available on request.
Stainless threads can gall when two stainless parts turn against each other dry. Name the mating part on the drawing, and we can suggest a lubricant or a different grade for one side.
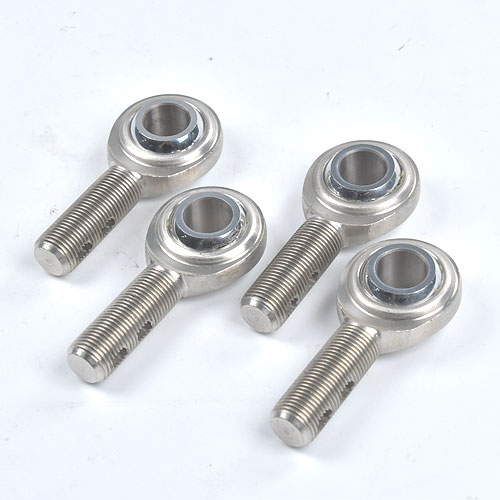 Rod Ends →
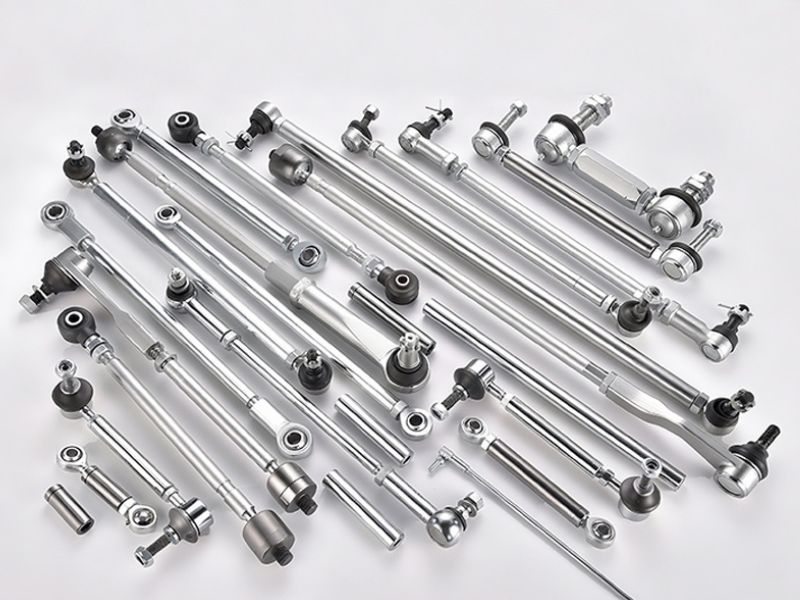
These product families start from a drawing, just like any CNC part. Each tile opens the product page with its sizes and grades.
Three short clips from the Profab YouTube channel. Each one loads when you press play.
We CNC machine your parts ourselves, so drawing questions reach the people who program the machines.
The same bracket drawing can be quoted in 304 for a dry frame and in 316L for a wet area. Quantity tiers appear on that quotation too.
There is no hard minimum, and prototype runs typically start around 100 pieces. A worn part can be measured and copied in stainless.
Send the drawing file, a sample, or a worn part. Add the grade, quantity, finish, and critical tolerances.
Engineering checks the geometry and the grade against the drawing. The quotation can show several quantity tiers.
Once the price is agreed, we confirm the final revision and requirements with you.
Sample parts are made for you to check before the full run starts.
The batch follows the approved sample. Parts ship by sea, air, or express courier.
We keep your approved drawing on file. A repeat order then starts from the same revision.
Short answers for engineers and buyers with a CNC part to quote.
We regularly machine 304, 316L, and 17-4PH. Other stainless grades, such as 303 and duplex 2507, are available on request. Tell us where the part works, and we suggest a grade.
Milled, turned, and drilled features are typically held to ±0.01 mm (about ±0.0004 in) where the drawing calls for it. The figure depends on the feature, the part size, and the grade, so we confirm it in the quotation.
Yes, 5-axis machining is available on request when a part needs it. Send a STEP file with the drawing so we can review the angled features.
Blocks, plates, brackets, and housings are milled because their features sit on flat faces. Round parts on one axis, such as pins and shafts, are turned. A turned part with flats or cross holes is turned first and milled afterward.
Yes. We measure a worn or corroded sample and quote a stainless copy. Tell us which grade the new part should be.
We offer passivation and electropolishing. Blackening, electroplating, and shot blasting are available on request. Name the finish on the drawing, because a finish changes the final size slightly.
There is no hard minimum. Prototype runs typically start around 100 pieces, and quantities vary by part.
Email the drawing or the sample details to [email protected]. Engineering reviews them and replies with a quotation.
Email Your Drawing