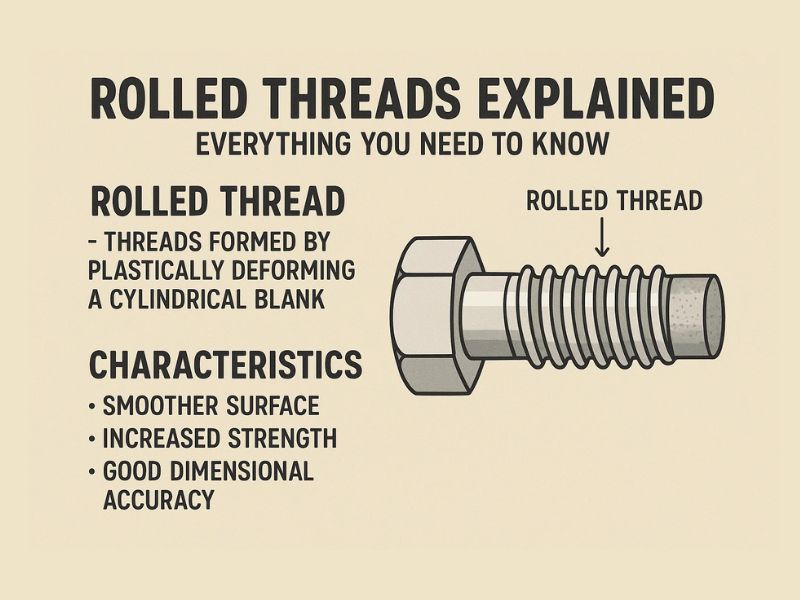
Rolled threads are formed by pressing a hardened die into a metal rod rather than cutting the thread form away. The metal grains flow along the thread shape instead of being severed, which is the source of the strength and fatigue advantage rolled threads have over cut threads. Here's how the process works, what it actually buys you, and when cutting is still the better call.
Rolled Threads Overview
What Are Rolled Threads
A hardened die presses onto a metal rod and rolls along it, shaping the thread form through plastic deformation rather than material removal. Because no metal is cut away, the grain structure that ran the length of the original rod continues to flow along the thread profile instead of being interrupted at each cut.
Thread rolling is covered by several UK/ISO standards, among them:
- BS 2517: definitions for use in mechanical engineering
- BS 3643: ISO metric threads
- BS 4827: ISO miniature threads
- BS 4846: ISO trapezoidal threads
- BS 21: pipe threads for tubes and fittings
Why Choose Rolled Threads
Rolling puts the surface layer into compression, and that residual compressive stress is what gives rolled threads their fatigue advantage over cut threads, cracks have to overcome the compressive stress before they can propagate. Rolled threads show up throughout stainless steel components: rod ends, ball joints, threaded rods, anywhere repeated load cycling makes fatigue life the limiting factor.
Thread Rolling Process
How Thread Rolling Works
The process starts with selecting the right material and forming it into straight bar stock. A thread rolling machine then shapes the threads onto each rod, followed by straightening and surface finishing, then cutting to final length. Each rod gets inspected before it ships. The result is threads that are exact and repeatable run to run, which matters for automotive and aerospace work where dimensional consistency isn't optional.
Tools and Machines
Different rolling equipment suits different production needs:
- Planetary thread rolling machines: the rod stays still while rollers form the threads
- Rotary thread rolling machines: similar function to planetary machines, used for comparable work
- Infeed rolling machines: round dies for short threads, efficient for high-volume runs
- Thrufeed rolling machines: form long threads in a single continuous pass, best suited to simple profiles
Material Suitability
Steel alloys, stainless steel, titanium, brass, bronze, aluminum, and high-temperature alloys all roll well, since the process needs a material that deforms plastically without cracking. Stainless steel is a particularly good fit for food, medical, and marine parts, where corrosion resistance matters as much as thread strength.
Rolled Threads: The Strength Case
Strength and Durability
Research on axial-infeed thread rolling measured yield strength improvements of roughly 41% and hardness improvements of roughly 39% at the thread root compared to the unformed material, a direct result of the grain refinement and compressive residual stress the rolling process creates. The cold working that produces this strength gain also hardens the surface, which is part of why rolled threads hold up better under repeated use than cut threads of the same nominal size.
Fatigue Resistance
Fatigue performance is where the difference between rolled and cut threads shows up most clearly in testing:
- Rolled threads fail less often in destructive fatigue testing than cut threads of the same spec
- The compressive residual stress from rolling raises tensile, shear, and fatigue strength together
- Aerospace fasteners with rolled threads consistently outperform cut-thread equivalents in qualification testing
For applications where a thread failure is a safety issue, this is the reason rolled threads are the default rather than an upgrade.
Speed and Cost
Thread rolling forms the thread in a single pass; cutting typically requires multiple passes to reach the same finished profile. That translates directly into throughput: rolling can run up to ten times faster than cutting, with less material waste per part. The economics favor rolling most clearly at volume, production runs in the thousands of pieces are where the per-part cost advantage is largest.
Surface Finish
Rolling burnishes the surface as it forms the thread, producing a smoother finish than cutting leaves behind:
| Thread Type | Surface Roughness (micro-inches Ra) |
|---|---|
| Rolled | 32 or less (commonly 8–24) |
| Cut | Rarely less than 63 (commonly 64–125) |
A smoother thread surface means less friction in service and less wear over the life of the fastener.
Applications of Rolled Threads
Die Materials
Die material selection depends on production volume and precision requirements:
| Material | Advantages | Applications |
|---|---|---|
| Carbide (Tungsten) | Very tough, wears slowly, high precision | Heavy-duty fasteners, aerospace parts, special threads |
| DC53 Steel | Tough, wear-resistant, easy to shape | High-volume standard fasteners |
| D55 Steel | Very hard, long-lasting, chip-resistant | Precision threads, abrasive materials |
| High-Speed Steel (HSS) | Economical, heat-tolerant, widely available | General-purpose dies for small to medium batches |
Industry Uses
Rolled threads are the default wherever fastener reliability under repeated stress matters: automotive, marine, medical, and industrial equipment all lean on the fatigue-life advantage rolling provides over cut threads.
When Not to Use Rolled Threads
Rolling isn't universally the right call. Tooling setup cost and lead time are higher than for cutting, which matters on short runs where the volume never gets high enough to recoup that cost. Rolling machines also have practical limits on thread length and diameter, and not every material deforms cleanly enough to roll without cracking, some will damage tooling or produce inconsistent threads if forced through the process.
Rolled Threads vs Cut Threads
Process Differences
| Feature | Rolled Threads | Cut Threads |
|---|---|---|
| Method of Formation | Cold-forming with a hardened die | Material removal with a cutting tool |
| Structural Impact | Grain flow continues through the thread | Grain flow is cut at each thread root |
| Precision | No tool marks; consistent from part to part | Can machine any diameter or pitch on demand |
| Installation Smoothness | Smoother due to the forming process | Can be rougher from tool marks |
| Damage Resistance | More resistant to fatigue and damage | Less resistant due to interrupted grain flow |
Performance Comparison
The mechanism behind the performance gap is straightforward: rolling keeps the grain structure continuous and puts the surface in compression, both of which resist crack initiation. Cutting interrupts the grain flow at the thread root, creating a natural starting point for fatigue cracks under repeated load. In applications with real cyclic stress, cut threads fail more often than rolled threads of the same nominal spec.
Conclusion
Rolled threads win on strength, fatigue life, surface finish, and per-part cost at volume, all because the process forms the thread rather than cutting it away. Cutting still has its place for short runs, oversized parts outside rolling equipment's range, and materials that don't deform cleanly. For stainless steel fasteners in automotive, marine, or medical service, rolled threads are the default for good reason.
Profab Machine manufactures stainless steel threaded components using rolling processes suited to the application, with the inspection to back it up.
FAQ
What makes rolled threads stronger than cut threads?
Rolling keeps the metal's grain structure flowing continuously along the thread shape instead of cutting through it, which improves both strength and fatigue resistance.
Can you use rolled threads for all types of metals?
Most ductile metals roll well, including stainless steel, titanium, and aluminum. Brittle materials that can't deform plastically without cracking aren't suited to the process.
How do you check the quality of rolled threads?
Thread ring gages and plug gages verify size and fit. Visual inspection checks for cracks, seams, and consistent grain flow before the part ships.
Are rolled threads more cost-effective for large orders?
Yes. The single-pass process and lower material waste bring the per-part cost down significantly at volume, which is where rolling's economics work best.
What industries benefit most from rolled threads?
Automotive, marine, medical, and aerospace, all fields where fastener reliability under repeated stress and corrosion resistance are both required.