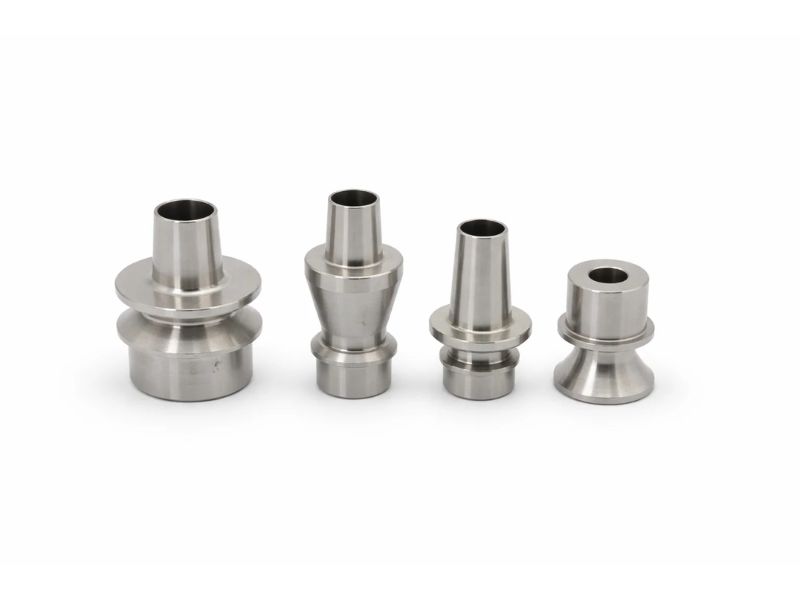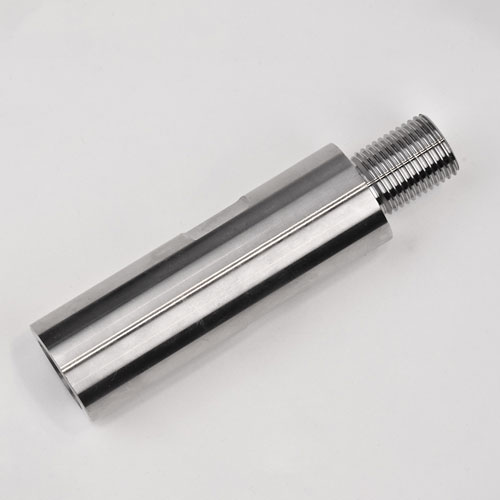
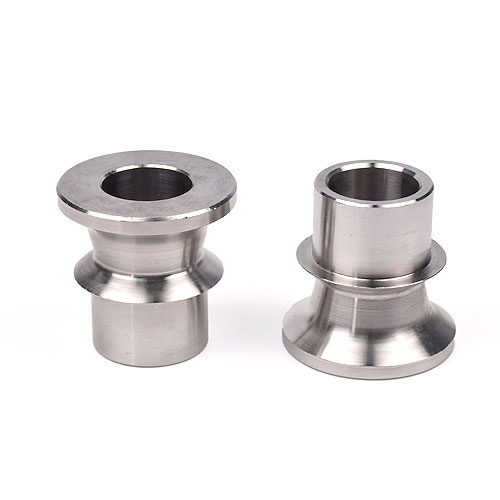
Custom rod end inserts in 304, 316L, and 17-4PH, with other grades on request. Press-in and threaded inserts that give a tube, a bar, or a bored body the internal thread of a rod end where welding is not wanted, left or right hand, made to your drawing or sample. For weld-in versions see weld-in bungs.
Applications: Hydraulic and Pneumatic Cylinders, Linkages in Automation, Composite and Thin-Wall Links, Marine Control Linkages.
The insert thread follows the rod end shank. These are common inch threads by rod end bore, and the common metric coarse threads. Left or right hand, and any other thread, are made to your drawing. Outside diameter, length, and the fixing method (press-in, bonded, or threaded) are set on your tube or bore.
| Thread | Standard | Pitch | Rod End |
|---|---|---|---|
| 1/2-20 | UNF | 20 threads per inch | 1/2 in bore |
| 5/8-18 | UNF | 18 threads per inch | 5/8 in bore |
| 3/4-16 | UNF | 16 threads per inch | 3/4 in bore |
| M6 | Metric coarse | 1.0 mm | Metric rod end |
| M8 | Metric coarse | 1.25 mm | Metric rod end |
| M10 | Metric coarse | 1.5 mm | Metric rod end |
| M12 | Metric coarse | 1.75 mm | Metric rod end |
Thread sizes follow the rod end shank and the outside diameter follows the tube or the bore, so name both.
| Form | How It Is Fixed | Typical Use |
|---|---|---|
| Press-in insert | Pressed into the tube or bore with an interference fit | Parts where a weld would distort the tube |
| Bonded insert | Held in the tube with an adhesive, often with a knurled or grooved body | Composite or thin-wall tubes that cannot be welded |
| Threaded insert | Screws into a tapped body | Adding a steel or stainless thread to a softer body |
| Stepped or shouldered insert | A body with a shoulder that seats on the tube end | Giving the insert a stop and a defined depth |
| Left and right hand set | One insert of each hand | Turnbuckle-style links that adjust by turning the tube |
Send a drawing, a DXF file, or a sample. Our engineers review the dimensions and the tolerance before cutting metal, and we CNC machine the part ourselves, so you deal directly with the factory.
We turn inserts to your tube or bore, with the thread cut on the same part, so the body seats square and the thread runs true.
Salt, moisture, washdown chemicals, and load drive the choice between 304, 316L, and 17-4PH. We confirm the grade against your drawing before production, and tiered pricing is available on larger orders.


A rod end insert is a threaded part fixed into a tube, a bar, or a bored body without a weld, so that a rod end can be screwed into it.
A weld-in bung is welded into the tube. An insert is pressed, bonded, or screwed in, so no weld heat reaches the thread. Choose a bung where the tube welds well, and an insert where it does not.
Match the thread of the rod end shank, for example 5/8-18 for a 5/8 rod end, and choose the same hand. A left and right hand pair lets the link adjust by turning the tube.
Choose 316L where the insert sees salt, chlorides, or chloride-based cleaning chemicals, because it resists pitting better than 304. Choose 304 for indoor, dry, or mildly humid service, where it costs less.
A quote request needs the thread size and hand, the tube outside diameter and wall or the bore, how the insert is fixed, the length, the grade, and the quantity. A drawing or a sample speeds it up.
If you already have drawings, email them to [email protected].
[email protected] ↗We use cookies to run this site, to measure how it is used, and to show relevant ads. You can accept all, reject all non-essential cookies, or choose by category. Privacy Policy